Get A Quote
Sep 28,2026
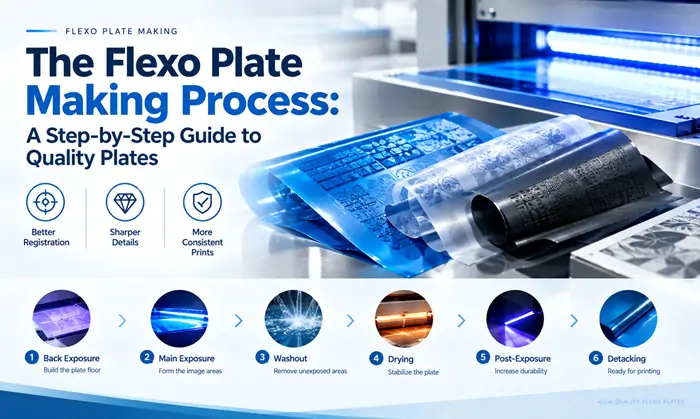
A flexographic printing plate is only as good as the process that made it. Back exposure, main exposure, washout, drying, post-exposure, and detacking—each step builds on the one before. If back exposure is too short, fine dots wash off. If main exposure is too long, reverse type fills in. If drying is incomplete, plates swell on press. This guide walks through the flexo plate making process step by step, explains what each stage controls, and identifies the most common errors that lead to plate failure.
To explore the available options, review the flexible printing plate configurations designed for different applications and plate-making systems.
What it does: Back exposure—also called pre-exposure or back flash—exposes the plate from the back side (substrate side) without vacuum. The UV light cures a thin layer of polymer across the entire plate back, creating the plate floor. This floor anchors the relief elements during washout.
What it controls: Back exposure determines two things: relief depth and dot anchoring. Relief depth is the distance between the plate floor and the top of the image areas. It is advisable to keep relief shallow if fine dots and lines are to be reproduced—this is achieved by using a longer back exposure. Dot anchoring refers to how firmly the raised dots are connected to the floor. Insufficient back exposure leaves dots under-anchored; they wash off during development. Excessive back exposure leaves the floor too close to the surface, causing the floor to print.
Common mistake: Skipping back exposure step tests. Back exposure time varies by plate type, thickness, and exposure unit condition. A step test is the only reliable way to dial in the correct time.
What it does: Main exposure—also called front exposure or imaging exposure—exposes the front of the plate through a film negative (analog) or a digital mask layer (digital). The UV light polymerizes the image areas, hardening them so they remain after washout.
What it controls: Main exposure shapes the relief by polymerization. All details of the image—lines, characters, halftone dots—are determined at this step and cannot be altered later. Main exposure time affects three critical characteristics:
Common mistake: Changing exposure time without re-running a main exposure test. The optimal main exposure time depends on the plate batch sensitivity, film negative quality, exposure unit condition, and the duration of back exposure.
A key decision within the plate-making process is whether the plate produces flat top dots or round top dots.
| Dot Type | How It Is Made | Key Characteristics |
|---|---|---|
| Round Top Dot | Light tube / conventional UVA exposure | Less stable under varying pressure; more dot gain; conventional process |
| Flat Top Dot | LED exposure or oxygen-inhibited digital process | Less sensitive to pressure variations; predictable and stable print runs; higher resistance to mechanical stress; better ink lay-down and density |
Flat top dots are produced when the digital plate-making process controls oxygen inhibition—for example, by using a digital mask layer and exposing in a reduced-oxygen environment, or by using LED exposure technology. The result is a flatter dot surface that maintains its size across a wider range of impression settings, reducing dot gain and improving print stability.
STRONG's digital flexo plates are designed to support flat top dot formation when adequate process equipment is used. The SF-DGS Digital Versatile Flexo Plate offers superior printing quality with sharper images, more open intermediate depths, finer highlight dots and less dot gain.
What it does: Washout—also called development—removes the unexposed, unpolymerized polymer from the plate. The plate is processed in a washout unit using solvent, thermal, or water-washable processing.
What it controls: Washout determines the final relief depth and the cleanliness of the plate floor. Insufficient washout leaves residual polymer that can cause scumming and plate contamination during printing. Excessive washout can damage fine relief elements.
Common mistake: Using the wrong washout solution or running the processor at the wrong speed. Washout speed and solution concentration must be matched to the plate type and thickness. If the processor is running too fast, unexposed polymer remains on the plate. If it runs too slow, fine dots may be over-developed and lost.
What it does: After washout, the plate is dried to remove absorbed solvent or water. Drying restores the plate to its original thickness and prepares it for post-exposure.
What it controls: Drying time and temperature affect plate dimensional stability. Incomplete drying leaves solvent trapped in the polymer, which can cause plate swelling, thickness variation, and registration drift during printing.
Common mistake: Reducing drying time to speed up plate production. The plate must be dried completely before post-exposure and mounting. Insufficient drying is one of the most common causes of plate thickness inconsistency.
What it does: Post-exposure exposes the plate to UV-A light to fully cure the polymer and strengthen the relief. Detacking—also called UVC finishing—exposes the plate to UVC light to eliminate surface tackiness, making the plate easier to handle and less likely to pick up dust or ink residue.
What it controls: Post-exposure strengthens the plate and improves its resistance to ink and solvent. Detacking eliminates the sticky surface that can cause plates to adhere to each other during storage or pick up contaminants on press.
Common mistake: Skipping post-exposure or detacking. Plates that are not fully post-exposed may swell excessively in ink and wear faster on press. Plates that are not detacked are difficult to handle and store.
What it does: The finished plate is inspected for relief depth, dot quality, and surface defects before it is mounted on press.
What to check:
For detailed quality control processes, explore the quality assurance processes that support consistent plate performance.
| Step | Analog Workflow | Digital Workflow |
|---|---|---|
| Imaging | Film negative required | Direct digital imaging (laser/UV-LED) |
| Back exposure | Same | Same |
| Main exposure | Through film negative | Through digital mask layer |
| Washout | Solvent, thermal, or water-washable | Solvent, thermal, or water-washable |
| Post-exposure | Same | Same |
| Detacking | Same | Same |
The key difference is the imaging step. Digital workflows eliminate film, which removes film shrinkage, dust, and handling errors. For a full comparison of digital and analog flexo plates, refer to our guide on digital vs analog flexo plates.
| Error | Effect | Prevention |
|---|---|---|
| Back exposure too short | Dots wash off; relief too deep | Run back exposure step test |
| Back exposure too long | Floor prints; relief too shallow | Verify relief depth |
| Main exposure too short | Dots not anchored; shoulders too weak | Run main exposure test |
| Main exposure too long | Reverse type fills in; shoulder too wide | Reduce exposure time incrementally |
| Washout insufficient | Scumming; residual polymer | Check processor speed and solution |
| Drying incomplete | Plate swelling; thickness variation | Increase drying time |
| Post-exposure skipped | Premature plate wear; swelling | Complete all post-processing steps |
For personalized guidance on plate-making parameters for your specific plate type and equipment, discuss your material and production requirements with the technical team.
Back exposure, also called pre-exposure, exposes the plate from the back side to create the plate floor. It determines relief depth and ensures firm anchoring of fine relief elements. Insufficient back exposure causes dots to wash off; excessive back exposure causes the floor to print.
Flat top dots are produced using LED exposure or oxygen-inhibited digital processes. They are less sensitive to pressure variations, produce more predictable print runs, and have better resistance to mechanical stress. Round top dots are produced with conventional light tube exposure and are more sensitive to impression changes.
Main exposure time depends on plate batch sensitivity, film negative quality, exposure unit condition, and back exposure duration. There is no single correct time. A main exposure test should be run whenever any of these variables change.
Skipping post-exposure leaves the plate incompletely cured. The plate may swell excessively in ink, wear faster on press, and lose fine detail. Post-exposure strengthens the polymer and improves resistance to ink and solvent.
Detacking, also called UVC finishing, eliminates surface tackiness on the finished plate. It makes the plate easier to handle, less likely to pick up dust or contamination, and prevents plates from sticking to each other during storage.
A properly dried plate returns to its original thickness. Measure the plate thickness with a micrometer after drying. If the thickness is greater than specification, drying is incomplete. Plates should be dried completely before post-exposure and mounting.
The flexo plate making process is a sequence of precisely controlled steps—back exposure, main exposure, washout, drying, post-exposure, and detacking. Each step affects the next, and errors at any stage show up on press as dot loss, fill-in, scumming, or plate swelling.
The most reliable way to avoid these problems is to run step tests for back and main exposure, control washout and drying parameters, and complete all post-processing steps. Digital plate-making workflows eliminate film-related variables, making the process more repeatable and reducing the risk of imaging errors.
If you are setting up a new plate-making process or troubleshooting recurring plate failures, review the available flexible printing plate configurations and discuss your specific plate type and equipment with the supplier.
Disclaimer: The information in this article is provided for general guidance only. Plate-making parameters—including exposure times, washout speed, drying temperature, and processing chemistry—vary by plate type, equipment, and production environment. Actual results should be verified through testing on your production equipment. Buyers should confirm specifications with their supplier before placing an order.
GET A QUOTE